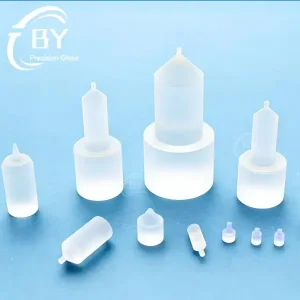
Core Laser & Optical Cavity Components
Engineered to withstand multi-kilowatt optical load densities, extreme thermal shocks, and chemically corrosive liquid coolant cycles.
Enterprise Procurement Dynamics & Industrial Status
Strategic shift toward integrated photonic packaging, ultra-high thermal conductivity ceramics, and defect-free synthetic substrates.
Thermal Management & Multi-kW Demands
Industrial photonics has transitioned from sub-kilowatt CW levels to 12kW-60kW continuous and petawatt-class ultrafast regimes. Global OEMs require laser cavity reflectors and quartz flow conduits with parts-per-billion impurity profiles to eliminate non-radiative absorptive center generation and micro-lensing failure.
Stringent Surface Roughness & LIDT
Laser Induced Damage Threshold (LIDT) mandates across EU and US medical and defense integrators enforce scratch-dig tolerances down to 10-5 / 20-10, with surface microroughness Ra < 0.5 nm. Sub-surface damage control via chemical-mechanical polishing (CMP) is now mandatory to avoid catastrophic dielectric breakdown.
Total Supply-Chain Resilience
Tier-1 procurement organizations are mitigating risk by consolidating single-process subcontractors into single-roof manufacturers. Direct consolidation of cold CNC ultrasonic machining, vacuum annealing, and precision oxyhydrogen glass-blowing eliminates the cumulative yield loss of multi-vendor processing.
Comprehensive Optical Subsystem Engineering
Addressing thermal distortion, acoustic wave damping, and spectral solarization across commercial and industrial deployments.
Solid-State Laser Cavities (DPSS & Flashlamp)
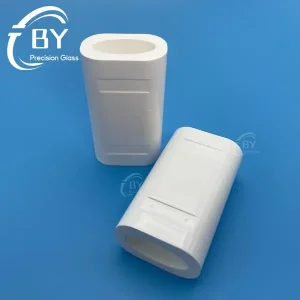
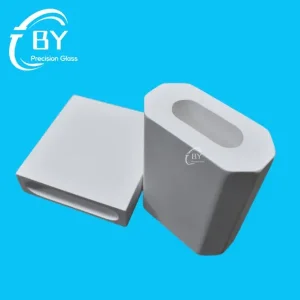
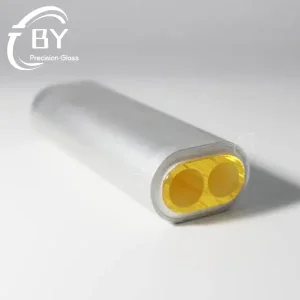
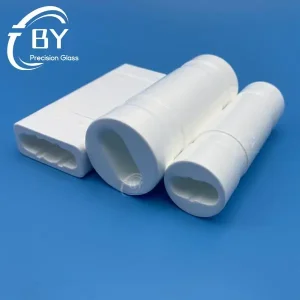
By pairing high-purity alumina (99.7% Al₂O₃) ceramic reflectors and samarium-doped (Sm³⁺) quartz flow tubes, we suppress parasitic 1064nm ASE (amplified spontaneous emission) and filter 400nm UV flash bands, extending operational crystal lifetimes past 15,000 continuous hours.
Medical IPL & Aesthetic Laser Systems
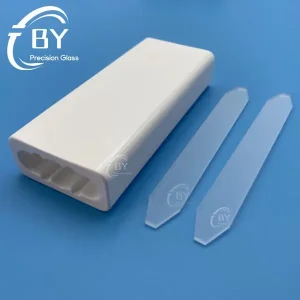
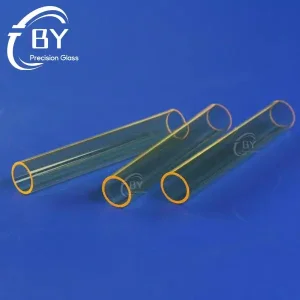
Intense Pulsed Light systems rely on our precision yellow-doped quartz jackets and sapphire wave guides with multilayer dielectric coatings to strip erythemal UVB/UVC radiation, delivering predictable dermal energy delivery and high burst pressure resistance under pulsed fluid loads.
Semiconductor Metrology & Wet-Process Tooling
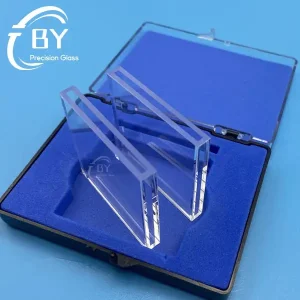
High-temperature diffusion boats, wafer carriers, and custom spectroscopy cells fabricated from synthetic JGS1 fused silica deliver zero-microbubble architectures capable of maintaining structural stability through 1100°C furnace processes and HF chemical etching washes.
| Material Substrate | Transmission Band | Thermal Expansion (CTE) | Bulk Reflectance / Index | Key OEM Application |
|---|---|---|---|---|
| JGS1 Synthetic Silica | 185 nm – 2,500 nm | 5.5 × 10⁻⁷ / °C | n = 1.458 @ 589nm | Deep UV Windows, QBH End Caps |
| Ceramic Laser Cavity (99.7% Al₂O₃) | Diffuse 500 – 1,200 nm | 7.2 × 10⁻⁶ / °C | > 97.5% @ 600–1064nm | Nd:YAG Pumping Cavities, DEKA/Candela |
| Spectralon-Grade PTFE | 250 nm – 2,500 nm | 1.0 × 10⁻⁴ / °C | > 99.2% Diffuse | High-Power Diode Pumping Enclosures |
| Samarium-Doped Quartz (Sm³⁺) | UV Cutoff + 1064nm Abs | 5.4 × 10⁻⁷ / °C | Select Band Filtration | Flashlamp Flow Tubes, Laser Heads |
| Optical Sapphire (Al₂O₃ Single Crystal) | 170 nm – 5,500 nm | 5.8 × 10⁻⁶ / °C | Mohs 9 Hardness | IPL Light Guides, High-Pressure Windows |
Technology Roadmap & Next-Gen Optical Matrix
Strategic engineering vectors guiding the next decade of multi-kilowatt processing, ultra-short pulse delivery, and coherent beam steering.
Low-Absorption Coatings & IBS Sputtering
Ion Beam Sputtering (IBS) deposition applied to JGS1 and sapphire substrates ensures ppm-level optical absorption loss, mitigating thermal focal shift in kilowatt single-mode fiber lasers and allowing sustained duty cycles without spatial wavefront distortion.
Additive Sintering & Complex Microchannel Geometries
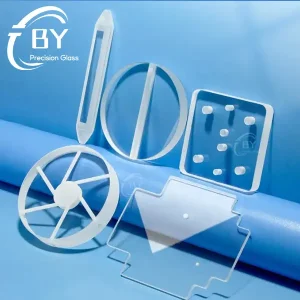
Micro-structured quartz flow plates and ceramic geometries now utilize multi-axis ultrasonic milling coupled with precision laser sintering. This delivers internal conformal liquid-cooling pathways that reduce thermal boundary layers by up to 42% compared to standard bore designs.
Automated In-Line Interferometric Quality Assurance
Phase-shifting Fizeau laser interferometry integrated with 3D coordinate-measuring machines (CMM) automates 100% surface form and stress-birefringence verification, assuring full mechanical interchangeability and zero lot-to-lot performance deviations.
Enterprise Compliance, Auditing & Tier-1 Support
End-to-end traceability, rigorous international material validation, and cleanroom handling protocols.
RoHS, REACH & Conflict-Free Compliance
Every synthetic fused silica blank, ceramic composite, and optical dopant complies with EU RoHS Directive 2011/65/EU and REACH (EC 1907/2006). Full spectral transmission and raw material melt lot documentation are archived for a minimum of 7 years.
Direct Engineering Hubs & DFM Turnaround
Our localized technical support framework connects your optical design engineers directly with our senior process team within 24 working hours. We provide full Design for Manufacturability (DFM) reviews covering chamfer optimization, stress mitigation, and cost-effective raw stock yield.
Class 1,000 / 10,000 Cleanroom Packaging
Laser optics and fluid-handling assemblies are ultrasonically degreased with high-resistivity deionized water, inspected under ultraviolet blacklight for organic residue, and hermetically sealed in anti-static, nitrogen-purged blister trays to eliminate transit particulates.
Frequently Asked Engineering Questions
Direct technical answers addressing physical tolerances, beam damage limits, material grades, and CAD handoffs.
What is the practical distinction between JGS1, JGS2, and JGS3 quartz substrates?
JGS1 is synthetic high-purity fused silica virtually free of bubbles and inclusions, delivering transmission from 185nm Deep UV through 2500nm with negligible fluorescence. JGS2 is fused quartz made from natural quartz crystal, optimal for visible optics (220nm–2500nm). JGS3 is produced with specialized vacuum melting to suppress the OH- absorption band at 2730nm, making it the industry choice for infrared systems up to 3500nm.
Why use Spectralon-grade PTFE reflectors instead of gold or silver metal coatings?
In high-power diode pumping chambers, metallic coatings (such as electroplated gold) suffer from pinhole oxidation, peeling from coolant turbulence, and high localized absorption spikes. Sintered PTFE delivers up to 99.2% diffuse Lambertian reflectance, total chemical inertness to deionized cooling water, and complete immunity to peeling or electrolytic corrosion.
How does samarium (Sm³⁺) doping protect solid-state laser crystals?
Samarium-doped glass selectively absorbs 1064nm photons while transmitting visible pump light from flashlamps. When used as cavity flow tubes in Nd:YAG lasers, it prevents transverse amplified spontaneous emission (ASE) from depopulating the upper laser state, eliminates parasitic oscillation, and blocks UV bands below 400nm that induce solarization defects in YAG matrices.
What tolerances can be routinely held on precision CNC glass machining?
For CNC ultrasonic grinding and precision glass milling, outer diameters, stepped bores, and slot dimensions are routinely held to ±0.01 mm (±10 µm). On high-precision optical flats and sapphire slider windows, flatness of λ/10 @ 632.8 nm and parallelism under 10 arcseconds are achieved with double-sided planetary lapping.
What CAD formats and parameters are needed for an actionable quote?
We work directly with STEP, IGES, DWG, DXF, and dimensioned PDF mechanical drawings. For optical and laser parts, please specify the required base material, operating wavelength, anti-reflective (AR) coating bandwidth, surface quality (MIL-PRF-13830B or ISO 10110), laser energy density (LIDT), and batch quantities.
Do you support rapid prototyping before volume OEM production?
Yes. Our engineering facility operates dedicated small-batch CNC and hot-working cells to fabricate prototypes (1–10 units) for feasibility testing. Full First Article Inspection (FAI) reports, including coordinate-measuring machine (CMM) data and spectrophotometric transmission curves, accompany each prototype batch prior to mass tooling rollout.
Specialized Laser Optics & Glass Ware Assemblies
Engineered for specialized clinical aesthetics, ultrafast beam delivery, spectrophotometry, and demanding high-temperature environments.