
High-Precision Quartz Plates & Optical Windows
Direct from our CNC lapping and polishing production floor. Built to DIN ISO 10110 standards with comprehensive interferometric metrology.
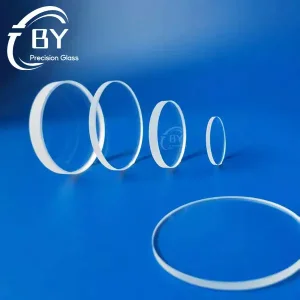
Wholesale Quartz Optical Windows for Semiconductor Lithography Equipment Suppliers, Factories
Configure & Inquire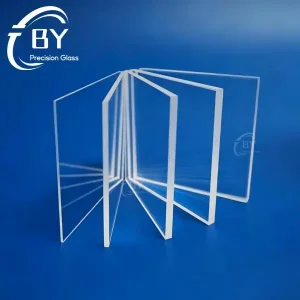
High-Quality JGS1 UItraviolet (UV) Grade Fused Silica Plate Supplier, Factory
Configure & Inquire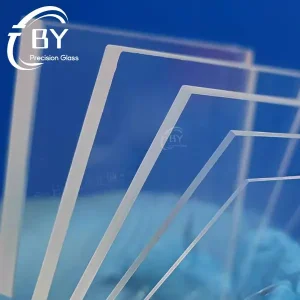
High-Quality Borosilicate Windows and Plates for Viewports Suppliers, Factory
Configure & Inquire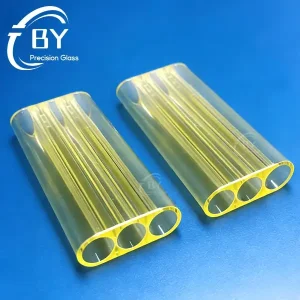
Wholesale Samarium-doped Quartz Triple Bore for Medical Laser Manufacturer, Supplier
Configure & Inquire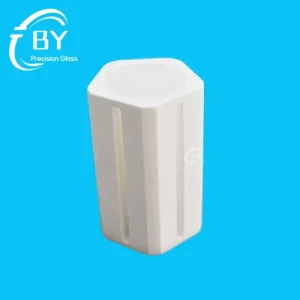
Wholesale Diffuse High‑Reflectivity PTFE Reflectors for Diode‑Pumping Chambers Suppliers, Factory
Configure & Inquire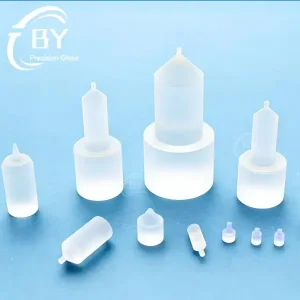
High-Quality Customized Quartz Fiber End Caps for QBH Manufacturer, Factory
Configure & Inquire
Wholesale Quartz Optical Windows for Semiconductor Lithography Equipment Suppliers, Factories
Configure & Inquire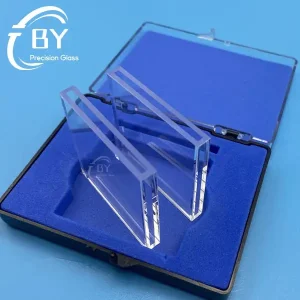
Wholesale Customize Quartz Cuvette for Spectrophotometer Supplier, Factory
Configure & InquireGlobal Industrial Landscape: Quartz Plates & Optical Windows
Critical sub-components enabling deep ultraviolet lithography, multi-kilowatt material processing, and space-based telemetry instrumentation.
In modern industrial photonics and semiconductor manufacturing, quartz plates and windows represent far more than protective transparent barriers. They are precision-engineered optical substrates designed to preserve wavefront integrity, withstand extreme thermal gradients, resist radiation-induced solarization, and handle mechanical pressure deltas in harsh operational environments. With the global photonics market transitioning toward higher optical power densities and shorter deep-ultraviolet (DUV) wavelengths, the tolerance thresholds for bulk purity, internal homogeneity, surface roughness, and transmitted wavefront distortion (TWD) have tightened by orders of magnitude.
A premier quartz plates and windows factory operates at the nexus of high-temperature material science and nanometer-scale cold finishing. In photolithographic steppers, excimer laser ablation systems, high-power solid-state lasers, and aerospace viewports, ordinary borosilicate or optical crown glasses fail rapidly due to localized thermal lensing, elevated thermal expansion coefficients (α > 3.3 × 10⁻⁶/K), or hydroxyl-driven absorption bands. Synthetic fused silica (JGS1 / Suprasil equivalent) and electrically fused quartz (JGS2 / JGS3 / Infrasil equivalent) solve these failure modes by providing an ultralow coefficient of thermal expansion (∼0.55 × 10⁻⁶/K), an extraordinarily broad optical transmission spectrum from 185 nm to 3,500 nm, and a laser-induced damage threshold (LIDT) exceeding 10–20 J/cm² at 1064 nm (10 ns pulse regimes).
Today's global procurement executives face dual pressures: maintaining uncompromising nanometer-level flatness (λ/10 to λ/20) while mitigating geopolitical supply chain vulnerabilities. As Western tier-one suppliers face extended backlogs spanning 16 to 36 weeks, advanced Chinese manufacturing hubs—anchored by facilities like Tianjin BY Photonics—have developed fully integrated vertically aligned capabilities. By consolidating chemical synthesis, raw ingot slicing, multi-axis ultrasonic CNC milling, double-sided planetary pitch polishing, and automated ion-assisted magnetron sputtering in a single location, modern factories provide reliable OEM scaling, sub-angstrom surface finishes (Ra < 0.2 nm), and rapid turnaround prototyping cycles.
$1.42B Global Market Valuation
Driven by semiconductor capital equipment investments, extreme ultraviolet (EUV) source scaling, and industrial high-brightness fiber laser installations expanding at 8.4% CAGR.
LIDT Thresholds > 15 J/cm²
Optical windows must resist irreversible thermal breakdown and dielectric rupture during multi-kilowatt continuous wave (CW) and ultrafast picosecond/femtosecond pulsed laser exposure.
Sub-Angstrom Super-Polishing
Eliminating mid-spatial frequency errors and surface sub-surface damage (SSD) to suppress forward light scatter and prevent chemical contamination trap sites in cleanroom operations.
Material Science & Optical Substrate Specifications
Comprehensive cross-grade reference matrix identifying transmission windows, hydroxyl [OH⁻] concentrations, and thermal thresholds across industrial quartz glass families.
| Material Classification | Primary Spectral Band | [OH⁻] Content | Index Homogeneity | Refractive Index (nd) | Max Service Temp | Typical OEM Application |
|---|---|---|---|---|---|---|
| JGS1 (Synthetic Fused Silica) Suprasil 1/2 Equivalent |
185 nm – 2,500 nm (DUV / UV) | ≤ 1,200 ppm | Δn ≤ 1–4 × 10⁻⁶ | 1.4585 | 1,100 °C | Lithography stepper optics, UV laser windows, high-purity cuvettes |
| JGS2 (Fused Quartz) Homosil Equivalent |
220 nm – 2,500 nm (Vis / Near-UV) | ∼ 150–200 ppm | Δn ≤ 5 × 10⁻⁶ | 1.4584 | 1,150 °C | Observation ports, laser protective debris shields, furnace viewports |
| JGS3 (IR-Grade Fused Quartz) Infrasil Equivalent |
260 nm – 3,500 nm (NIR / SWIR) | ≤ 5 ppm | Δn ≤ 6 × 10⁻⁶ | 1.4581 | 1,200 °C | Infrared thermography windows, pyrometry, gas sensing analytical cells |
| Corning 7980 (HPFS) High-Purity Silica |
190 nm – 2,100 nm (DUV / Vis) | ∼ 800–1,000 ppm | Δn ≤ 1–2 × 10⁻⁶ | 1.4585 | 1,050 °C | Interferometer reference flats, aerospace telescope mirrors, DUV beam splitters |
| Borosilicate (Borofloat 33) Engineered Glass |
350 nm – 2,500 nm (Vis / NIR) | N/A | Commercial Grade | 1.4714 | 450 °C | Pressure viewports, chemical sight glasses, commercial explosion-proof barriers |
| Optical Sapphire (Al₂O₃) Single Crystal C-Plane |
170 nm – 5,500 nm (Broadband) | 0 ppm | Anisotropic Birefringent | 1.7680 | 1,800 °C | Extreme pressure deep-sea viewports, IPL light guides, supersonic radomes |
Localized High-Performance Application Scenarios
Examining the engineering demands of precision quartz plates and windows across critical mission-critical industries.
Semiconductor Photolithography
DUV excimer stepper systems operating at 248 nm (KrF) and 193 nm (ArF) require JGS1 synthetic fused silica windows with near-zero bubble/inclusion classes (ISO 10110 Class 0/0). Substrates eliminate optical solarization, compaction, and flare under prolonged intense UV flux.
Ultra-High Power Industrial Lasers
Fiber laser cutting and welding heads operating at 10 kW to 30 kW utilize JGS1 and high-purity JGS2 protective cover slides. Ion-beam sputtered (IBS) anti-reflective coatings hold absorption below 5 ppm, preventing destructive thermal lensing and focus shifting.
Aerospace & Hypersonic Viewports
Optical observation ports installed on aerospace test vehicles, atmospheric re-entry capsules, and cryogenic wind tunnels must withstand extreme delta-T conditions (>1,000 °C instantaneous shock) while maintaining hermetic seal integrity in ConFlat (CF) and ISO vacuum flanges.
Biomedical Spectrophotometry
Clinical diagnostic instrumentation, flow cytometry view cells, and PCR analytical devices demand zero-autofluorescence quartz windows and cuvette windows. Chemically inert surfaces prevent sample cross-contamination, ensuring absolute repeatability during molecular assays.
Integrated Manufacturing Superiority & Agile Engineering
How domestic vertical integration eliminates multi-tier markups and long lead-times without compromising metrological rigor.
A primary bottleneck in global optical engineering procurement has historically been fragmented subcontracting. A conventional procurement workflow often involves sourcing raw ingots from one refiner, shipping blanks to a dedicated cutting shop, outsourcing pitch polishing to an optical artisan, and transshipping polished plates across borders for optical thin-film coating. Each hand-off introduces cumulative micro-defects, edge chipping, subsurface fractures, and uncontrollable schedule slippage.
At Tianjin BY Photonics Co., Ltd., this fragmentation is eliminated through a consolidated, under-one-roof production model established over 15 years of operational maturation. Situated in Tianjin's industrial manufacturing corridor with immediate access to raw high-purity quartz precursors and international logistics hubs, our facility manages cold machining, oxyhydrogen flame processing, ultrasonic CNC contouring, double-sided planetary lapping, and cleanroom vacuum packaging within a continuous traceable QA environment.
Direct Material Traceability
We maintain multi-ton inventories of inspected JGS1, JGS2, JGS3, high-purity borosilicate, and optical sapphire ingots. Each material batch is spectrally characterized via UV-Vis-NIR spectrophotometry to verify cutoff wavelengths and OH concentrations prior to cutting.
70% Shorter OEM Lead Times
While European and North American optical foundries quote standard fulfillment lead times of 12 to 24 weeks, our agile double-sided batch lapping clusters and multi-spindle CNC platforms routinely deliver customized prototype batches within 10 to 15 working days.
100% Metrological Verification
Our quality control laboratory is equipped with Zygo phase-shifting laser interferometers (632.8 nm), non-contact white light interferometry for nanometer surface roughness, and automated vision measurement systems verifying dimensional tolerances down to ±0.01 mm.
Compliance Standards & Class 1000 Cleanroom Packaging
Fulfilling stringent global regulatory benchmarks across North American, European, and Asian optical instrumentation markets.
ISO 10110 Optical Drawing Adherence
Our engineering division directly interprets all international optomechanical drafting standards. Every critical notation—from 0/ (stress birefringence), 1/ (bubbles and inclusions), 2/ (inhomogeneity and striae) to 5/ (surface form tolerance)—is mapped into production routing sheets.
RoHS & REACH Compliance
All quartz, fused silica, optical coatings, and polishing slurries utilized within our production facility are guaranteed free from restricted heavy metals, lead, cadmium, hexavalent chromium, and SVHC chemicals, ensuring frictionless customs clearance globally.
Hermetic Export Packaging
Precision optics are ultrasonically cleaned through multi-stage DI-water cascades, dried in HEPA laminar flow benches, and sealed in inert nitrogen-purged membrane boxes or lint-free lens tissue inside Class 1000 cleanrooms to eliminate transit contamination.
Frequently Asked Questions: Technical Specifications & Sourcing
In-depth technical answers addressing material selection, fabrication tolerances, laser thresholds, and design for manufacturability (DFM).
Laser Cavities, Precision Machining & Flow Assemblies
Advanced quartz fabrication, capillary redrawing, and custom reflective cavities supporting global laser system builders.
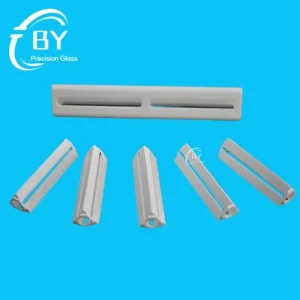
High-Quality Diode‑Pumping Chamber Diffuse Reflectors PTFE‑based Supplier, Suppliers
Configure & Inquire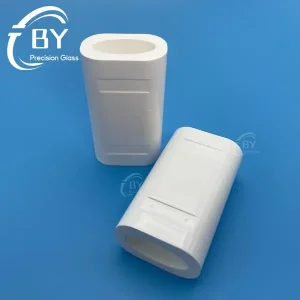
High-Quality Ceramic Cavities For Nd YAG Laser Supplier, Factories
Configure & Inquire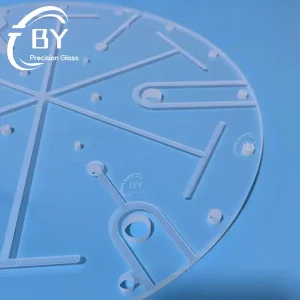
High-Quality Custom Precision Quartz Glass Fabrication Supplier, Suppliers
Configure & Inquire
High-Quality Custom Quartz Glass Components for Vacuum Coating Supplier, Factories
Configure & Inquire
Custom Fiber Optic Glass Ferrules Supplier, Factories
Configure & Inquire
High-Quality Custom Precision Quartz Capillary Tubes Manufacturers, Suppliers
Configure & Inquire
Custom UV Block Yellow Quartz Tube for IPL Lamp Flow Handle Manufacturer, Factories
Configure & Inquire
High-Quality Candela Laser Distance Gauge Slider Windows With coating 755 and 1064nm Suppliers, Factories
Configure & InquireSubmit Drawings for a Rapid Technical Review
Connect directly with senior optical manufacturing engineers. Send your CAD models (STEP, IGES, DWG) or dimensioned 2D PDF blueprints with specified scratch-dig, flatness, and wavelength requirements for a comprehensive DFM assessment within 24 hours.