
High-Precision Engineered Quartz Components
Manufactured from high-purity synthetic fused silica and electro-fused natural quartz (JGS1, JGS2, JGS3), achieving superior thermal shock resistance, extreme UV-to-IR transmittance, and zero particulate flaking.
Evolution of High-Purity Fused Quartz Machining in Advanced Manufacturing
A systematic examination of mechanical behavior, thermal kinetics, and sub-micron fabrication methodologies for extreme industrial environments.
Material Purity & Lattice Integrity
Silicon Dioxide (SiO₂) in its non-crystalline vitreous state exhibits anomalous thermal and chemical properties. Fused silica synthesized through silicon tetrachloride vapor oxidation yields impurity concentrations below 5 ppb for metallic elements, eliminating unwanted UV absorption and dielectric loss in radio-frequency plasma chambers.
- Metallic Contaminants: < 0.1 ppm total
- OH Radicals: 1 ppm (Dry) to 1200 ppm (UV)
- Refractive Index Homogeneity: Δn ≤ 2×10⁻⁶
Brittle Fracture Mitigation
Machining non-ductile glass substrates necessitates controlled crack propagation modes. Utilizing high-frequency ultrasonic-assisted CNC grinding alongside optimized diamond tool matrices suppresses subsurface damage (SSD). Crack depths are constrained to under 1.5 μm, avoiding delayed catastrophic fracture under high-pressure thermomechanical stress.
- Ultrasonic Frequency: 20–40 kHz Resonance
- Diamond Grain Size: D15 to D46 Electroplated
- Edge Chipping Limit: ≤ 0.02 mm Controlled
Thermomechanical Invariance
With an extraordinarily low thermal expansion coefficient of 5.5 × 10⁻⁷ / °C between -50°C and 1000°C, quartz components resist severe thermal transients that cause crystalline ceramics or borosilicate glasses to fail. Components remain dimensionally stable within sub-micron parameters during cyclical wafer heating and cooling protocols.
- Thermal Shock Resistance: ΔT = 1100°C into Water
- Softening Point: ~1683°C (Annealing 1120°C)
- Dielectric Constant: 3.75 @ 1 MHz
Global Enterprise Sourcing Criteria & Total Cost of Ownership (TCO)
Enterprise procurement divisions in the semiconductor, aerospace, and biomedical sectors manage strict supply chain risks. We deliver structural value by addressing core procurement hurdles directly.
Full Ingot Traceability
Every fabricated batch includes raw boule lot validation, verifying glow discharge mass spectrometry (GDMS) purity, bubble class (DIN 3140 / ISO 10110), and residual stress birefringence under polarized inspection.
DFM Engineering Response
Our application engineering department returns comprehensive Design for Manufacturability (DFM) analyses within 24 hours, proposing tolerance rationalization that minimizes machining cycle time and cuts scrap risk.
Class 100/1000 Packaging
Cleanroom processing stops airborne particulates from settling on machined quartz surfaces. Cleaned in ultrasonic deionized water baths (18 MΩ·cm) and sealed in anti-static multi-layer cleanroom pouches ready for vacuum loading.
Supply Continuity & Dual Sourcing
Strategic buffers of certified optical fused silica ingots ensure our customers are shielded from international raw silica logistics bottlenecks, keeping lead times steady for repeat high-volume OEM releases.
Macro Industry Engineering Solutions
Tailored quartz machining architectures engineered to withstand challenging thermal, corrosive, and optical service requirements across modern scientific disciplines.
Semiconductor & Photolithography
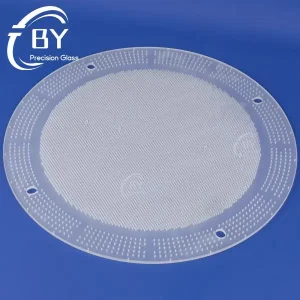
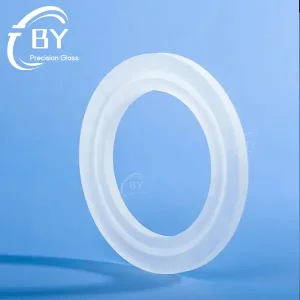
Quartz gas showerheads, etch rings, wafer lift pins, and diffusion boats operating in fluorine- or chlorine-based plasma. Exceptional chemical inertness prevents chamber erosion, extending mean-time-between-cleans (MTBC) on production wafer lines.
- Plasma Etch Resistance: CF₄, NF₃, Cl₂ Chemistries
- Micro-Nozzle Hole Tolerances: ±0.01 mm
- Particle Flaking Reduction: Acid Fire Polished
Photonics & High-Power Lasers
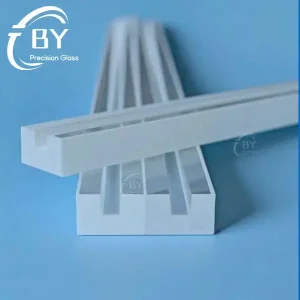
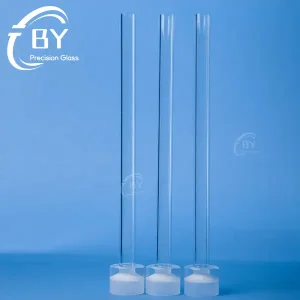
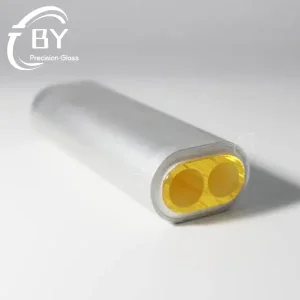
Fiber end-caps for high-power QBH combiners, custom triple-bore Candela laser pump cavities, laser flow tubes, and low-absorption debris shields capable of handling gigawatt-level peak optical power densities without thermal lensing.
- Laser Damage Threshold (LIDT): > 45 J/cm² @ 1064nm, 10ns
- Bulk Absorption: < 3 ppm/cm at 1064 nm
- Multi-Bore Concentricity: Runout < 0.02 mm
Biomedical & Microfluidics
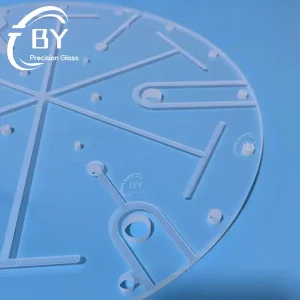
Quartz spectrophotometer cuvettes, capillary electrophoresis flow cells, and microfluidic chips requiring deep UV transmission (down to 185 nm) and near-zero background autofluorescence for DNA sequencing and single-molecule fluorescence detection.
- Autofluorescence: Undetectable under 365/488 nm excitation
- Optical Path Length Precision: ±0.005 mm
- Diffusion Bonding: Direct adhesive-free quartz fusion
Full-Spectrum Precision Glass Machining Workflows
Combining cold abrasive CNC machining, high-temperature thermal flame working, laser ablation, and optical polishing in one integrated factory.
5-Axis Ultrasonic CNC Milling
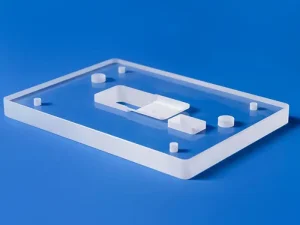
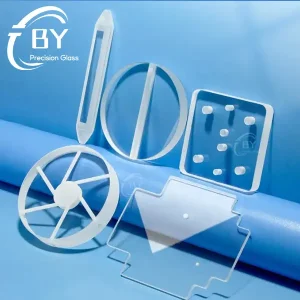
Multi-axis kinematic control for milling complex pockets, curved surfaces, bevels, and micro-hole arrays. Ultrasonic assistance lowers cutting force by up to 60%, limiting tool chatter and subsurface fracturing in hard, brittle quartz and sapphire substrates.
Oxyhydrogen Thermal Flame Fusion
High-purity hydrogen-oxygen flame welding for joining complex quartz components—such as wafer diffusion boats, cooling jackets, and vacuum flanges. Parts undergo programmed annealing up to 1150°C to release internal lattice stresses.
Double-Sided Optical Lapping & CMP
Planar double-sided planetary polishing achieving surface roughness Ra < 0.5 nm and surface figure accuracy up to λ/10 @ 632.8 nm. Clean chemomechanical polishing (CMP) methods protect against sub-surface scratches and embedded abrasives.
Optical & Thermal Fused Quartz Grade Guide
A reference table comparing optical transmission, trace hydroxyl (OH⁻) content, and typical engineering uses across standard fused quartz and fused silica grades.
| Material Designation | Origin & Synthesis Process | Transmission Bandwidth | Hydroxyl [OH⁻] Content | Primary Industrial Applications |
|---|---|---|---|---|
| JGS1 / Fused Silica | Synthetic SiCl₄ Vapor Phase Hydrolysis | 185 nm – 2500 nm (Deep UV) | < 1200 ppm (High OH) | Deep-UV lithography, Excimer laser windows, microfluidics, spectroscopy cuvettes |
| JGS2 / Fused Quartz | High-purity natural quartz crystal, oxyhydrogen melted | 220 nm – 2500 nm (UV-Vis) | < 30 ppm (Standard) | Semiconductor viewports, furnace sight glasses, optical flats, laser flow tubes |
| JGS3 / IR Quartz | Natural quartz melted under vacuum electro-fusion | 260 nm – 3500 nm (Infrared) | < 5 ppm (Water-free IR) | Mid-IR thermal pyrometry windows, infrared heaters, CO₂ laser cavity components |
| Corning 7980 / HPFS | Direct synthetic vapor deposition | 185 nm – 2200 nm (High Homogeneity) | ~800–1000 ppm | Sub-micron microlithography optics, interferometer reference flats, beam splitters |
| Doped Quartz (Sm/Ce) | Fused silica with Samarium or Cerium oxide additions | Filters 1064nm parasitic / UV block | Custom Doped Matrix | Solid-state Nd:YAG flashlamp flow tubes, aesthetic medical IPL filtration tubes |
Global Compliance, Quality Control & Engineering Support
Our quality verification processes and international regulatory alignment ensure reliable parts delivery across global supply chains.
Dimensional & Surface Metrology
Every critical batch undergoes verification using Zeiss multi-sensor Coordinate Measuring Machines (CMM), Zygo laser interferometers (measuring transmitted wavefront distortion and surface figure to λ/20), and Taylor Hobson optical profilometers for sub-nanometer surface roughness checks.
Material Certificates & COC
Shipments arrive complete with Certificate of Conformance (COC), GDMS purity analysis, spectrophotometer transmission scans, and dimensional inspection sheets detailing all drawing tolerances.
Regulatory & Cleanliness Standards
Full compliance with RoHS 3 (EU 2015/863), REACH (EC 1907/2006), and Conflict Minerals regulations. Cleanroom multi-stage ultrasonic degreasing, HF surface passivating etch, and double vacuum sealed packaging ready for ISO Class 5 cleanrooms.
Engineering Roadmap & Next-Generation Capabilities
Adapting quartz machining technologies to keep pace with shrinking nodes, rising laser powers, and tighter micro-mechanical specifications.
Plasma-Assisted Polishing (PAP)
Deploying atmospheric pressure plasma jet polishing and magnetorheological finishing (MRF) to eliminate surface residual stresses and bring surface roughness down to Ra < 0.15 nm for advanced high-power DUV/EUV optical elements.
Femtosecond Laser-Induced Etching (FLIE)
Employing selective chemical etching driven by femtosecond lasers to create true 3D microfluidic paths, sub-micron channels, and high-aspect-ratio holes (> 50:1) inside monolithic fused silica without mechanical micro-cracking.
300mm / 450mm Thermal Tool Ware
Expanding our CNC envelope and cleanroom automated annealing ovens to manufacture monolithic fused silica rings and showerheads exceeding 650 mm in outer diameter for 300mm advanced packaging and next-gen semiconductor processes.
Frequently Asked Engineering & Sourcing Questions
Detailed technical answers addressing design tolerances, thermal thresholds, and custom machining options for quartz components.
What is the standard machining tolerance for custom CNC quartz parts?
For standard CNC grinding, we typically maintain dimensional tolerances of ±0.05 mm (±0.002"). For high-precision requirements, multi-axis ultrasonic CNC finishing and double-sided planetary lapping can achieve tolerances down to ±0.002 mm (±0.00008"), hole pitch accuracy within ±0.005 mm, and surface flatness to λ/10 @ 632.8 nm.
How do you choose between JGS1, JGS2, and JGS3 quartz grades?
Select JGS1 (synthetic fused silica) for deep ultraviolet applications down to 185 nm or high-power laser systems where high optical transmission and low autofluorescence are required. Choose JGS2 for general semiconductor, furnace, and optical sight glass applications operating across visible wavelengths (220–2500 nm). Specify JGS3 (water-free fused quartz) for mid-infrared instrumentation and pyrometry up to 3500 nm, where OH absorption bands at 2730 nm must be avoided.
Can quartz parts handle thermal shock and high-temperature cycling?
Yes. Fused quartz features an exceptionally low coefficient of thermal expansion (5.5 × 10⁻⁷ / °C). Properly annealed quartz components can be heated to 1100°C and rapidly water-quenched without thermal shock failure. Continuous operational temperatures reach up to 1150°C, with short excursions permissible up to 1300°C before devitrification (cristobalite crystal growth) begins.
How do you prevent micro-cracks and subsurface damage during cutting?
We mitigate subsurface damage through controlled ductile-regime ultrasonic machining, fine-grit diamond tooling with multi-stage grit progression (from coarse roughing to D15 finishing), low feed rates, and constant coolant flow. Post-machining, parts undergo light acid etching (HF/HNO₃) or oxyhydrogen flame fire-polishing to relieve residual tensile stresses and smooth the edge profile.
Which CAD formats are supported for manufacturing feasibility reviews?
We accept 3D models in STEP (.stp), IGES (.igs), and Parasolid (.x_t) formats, paired with dimensioned 2D engineering drawings in PDF, DWG, or DXF showing critical datum references, GD&T callouts, surface roughness (Ra), and scratch-dig requirements. Complete engineering reviews and DFM assessments are returned within 24 working hours.
What optical coatings and post-machining finishes can you supply?
Beyond precision mechanical cutting and lapping, we offer in-house optical coatings, including single and multi-layer Anti-Reflective (AR) coatings, high-reflectivity dielectric dielectric mirror coatings, and metalized coatings (Gold, Aluminum, Chrome). Surface finishes range from commercially frosted (fine ground Ra 1.6 μm) to laser-grade polished (Ra < 0.5 nm, Scratch-Dig 10-5).
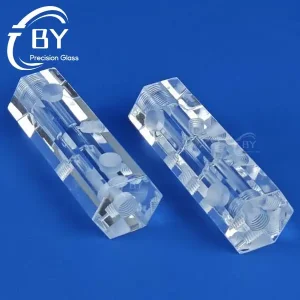
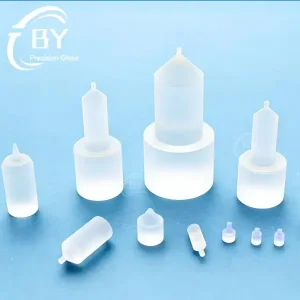
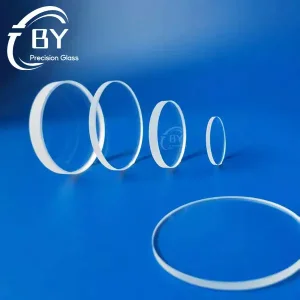
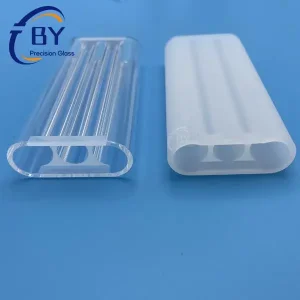
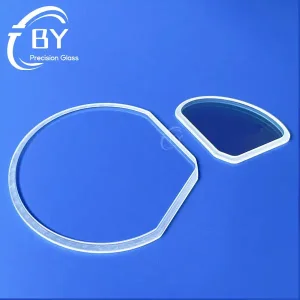
Precision Laser, Optical & Specialty Quartz Fabrications
Explore additional manufactured geometries engineered for laser cavity filtration, high-pressure sight viewing, fiber coupling, and lithography optics.
Submit Your Drawing for Engineering Feasibility Review
Send your STEP, IGES, or dimensioned PDF drawings directly to our engineering team. Our senior process engineers evaluate geometry, material grades (JGS1/JGS2/JGS3), and tolerance callouts, returning an actionable manufacturability report within 24 working hours.