
Specialized Precision Optics & Flowtube Assemblies
Engineered to exact geometric tolerances, laser-induced damage thresholds (LIDT), and custom dopant concentrations for photonics, aesthetic medical heads, and semiconductor tools.
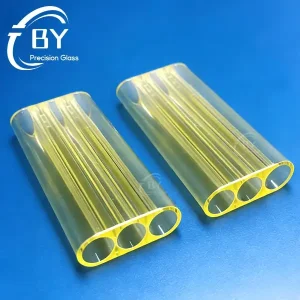
Wholesale Samarium-doped Quartz Triple Bore for Medical Laser Manufacturer, Supplier
Explore Product
Wholesale Fluorine-Doped Fused Silica Capillary Tube Manufacturer, Factories
Explore Product
High-Quality Diffuse Reflectors Made of Spectralon‑Grade PTFE for Diode‑Pumping Chambers Manufacturer, Suppliers
Explore Product
Custom Packed Laser Cavity Flowtubes for Laser Head Manufacturers, Suppliers
Explore Product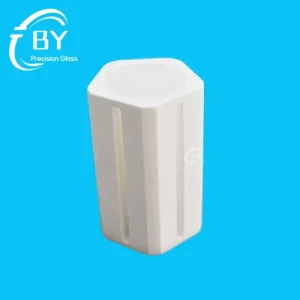
Wholesale Diffuse High‑Reflectivity PTFE Reflectors for Diode‑Pumping Chambers Suppliers, Factory
Explore Product
High-Quality Borosilicate Windows and Plates for Viewports Suppliers, Factory
Explore Product
Wholesale Ceramic Cavity Reflector use for DEKA Laser Manufacturers, Supplier
Explore Product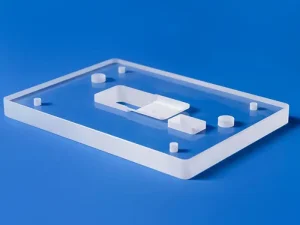
High-Quality Factory Supply Precision Quartz Glass Machining Plate Supplier, Suppliers
Explore ProductGlobal Sapphire Crystal Market & Crystallographic Physics
An in-depth analysis of high-purity single-crystal alpha-alumina (α-Al2O3) growth dynamics, plane orientations, mechanical hardness, and high-transmission broadband windows.
Synthetic sapphire crystal, chemically known as corundum or single-crystal aluminum oxide (α-Al2O3), occupies a dominant status across advanced modern engineering. Characterized by a trigonal crystal structure with hexagonal lattice symmetry, it exhibits an extraordinary combination of thermal, optical, mechanical, and chemical properties that cannot be matched by conventional optical fused silica, borosilicate, or optical glasses. As technological applications migrate toward extreme operating conditions—such as deep-ultraviolet (DUV) lithography, high-power infrared laser tracking, aerospace sensor pods, deep-subsea viewports, and high-pressure chemical reactors—the global commercial and industrial demand for precision-machined sapphire components continues to experience exponential expansion.
Crystallographic Plane Orientations and Anisotropy
Unlike isotropic amorphous glasses, single-crystal sapphire exhibits distinct anisotropic behavior. Optical, mechanical, and dielectric properties vary predictably based on the crystallographic cut angle. Qualified suppliers and precision factories must understand these characteristics to advise procurement and optical engineering teams during drawing specification:
C-Plane (0001)
Zero Birefringence Normal to Surface. Grown along the c-axis, C-plane sapphire exhibits no optical birefringence when light propagates parallel to the optical axis. It is the primary choice for optical windows, laser viewports, and GaN/InGaN LED epitaxy substrates.
A-Plane (11-20)
Uniform Dielectric Properties. Features uniform dielectric constants and low lattice mismatch for specific microwave devices, optical waveplates, and hybrid microelectronic packaging substrates requiring high mechanical rigidity.
R-Plane (1-102)
Silicon-on-Sapphire (SOS). The favored orientation for hetero-epitaxial silicon deposition in rad-hard military integrated circuits, high-frequency telecommunication RFICs, and piezoelectric transducer sensor diaphragms.
M-Plane (10-10)
Non-Polar Plane Epitaxy. Crucial for advanced non-polar and semi-polar optoelectronic structures, solid-state lighting arrays, and specialized laser diodes requiring high carrier recombination efficiency.
When utilizing sapphire in polarized optical trains (such as polarization-maintaining laser systems or imaging polarimeters), non-C-plane cuts act as uniaxial waveplates, inducing severe phase retardation and wavefront distortion. Specifying orientation alignment tolerance (e.g., ±0.5° or ±0.1° to the c-axis via X-ray diffractometry) is imperative for polarized performance.
| Material Type | Transmission Bandwidth | Knoop Hardness (kg/mm²) | Young's Modulus (GPa) | Thermal Shock Parameter | Common Applications |
|---|---|---|---|---|---|
| Monocrystalline Sapphire (α-Al2O3) | 170 nm – 5,500 nm | 1,800 – 2,200 (Mohs 9) | 345 – 435 | Exceptional (>10× quartz) | Extreme viewports, laser debris shields, IR domes, wafer carriers |
| JGS1 Synthetic Fused Silica | 185 nm – 2,500 nm | 450 – 600 (Mohs 6.5) | 72 | Moderate | DUV lithography optics, excimer lasers, spectroscopy cuvettes |
| JGS2 Optical Fused Quartz | 220 nm – 2,500 nm | 450 – 580 (Mohs 6) | 70 | Moderate | Sight glasses, flow tubes, semiconductor furnaces, lamp tubes |
| JGS3 Low-OH Fused Quartz | 260 nm – 3,500 nm | 450 – 580 (Mohs 6) | 70 | Moderate | Mid-infrared windows, heater elements, analytical detectors |
| Borosilicate Glass (e.g., Pyrex) | 350 nm – 2,500 nm | 400 – 500 (Mohs 5.5) | 64 | Low-to-Medium | Low-temperature laboratory sight glasses, capillaries, fluidic covers |
Chinese Factory Efficiency Advantages & Process Integration
How state-of-the-art Kyropoulos crystal growth facilities, diamond multi-wire slicing, and integrated CNC clustering eliminate Western lead-time bottlenecks.
Mega-Boule Kyropoulos (KY) Growth
Domestic Chinese growth facilities operate advanced automated induction-heated furnaces capable of pulling high-purity sapphire boules exceeding 200 kg to 500 kg with minimal dislocation density. This mass scale drives down the raw material ingot cost per square millimeter, creating an unmatched cost baseline for global tier-one OEM suppliers.
Diamond Multi-Wire Kerf Slicing
Traditional inner-diameter (ID) sawing produces severe subsurface micro-fractures and substantial kerf material waste. Chinese factories utilize ultra-high-speed multi-wire diamond slicing systems that slice hundreds of sapphire wafers simultaneously with kerf losses under 180 μm and Ra surface roughness below 0.2 μm, dramatically shortening subsequent planetary lapping cycles.
Planetary CMP Chemical Polishing
Chemical Mechanical Planarization (CMP) combining colloidal silica with tailored alkaline chemistry removes the amorphous Beilby layer. This process delivers true atomic-level flatness (λ/10 @ 632.8 nm) and surface scratch-dig tolerances exceeding 10-5 per MIL-PRF-13830B or ISO 10110 standards, completely eliminating subsurface damage (SSD).
Beyond sheer equipment scale, the decisive competitive advantage of Chinese sapphire manufacturers resides in vertical supply chain localization. Within optical processing clusters such as the Tianjin and Yangtze River Delta industrial belts, the entire life-cycle of raw high-purity alumina (5N+ precursor), graphite/molybdenum crucibles, high-precision five-axis ultrasonic CNC milling centers, and specialized diamond-resin grinding consumables is interconnected within a tight geographic radius.
Consequently, prototype fabrication cycles that typically consume 8 to 12 weeks among European or North American machine shops are compressed to 10 to 15 business days in China, while maintaining stringent ISO 9001 and AS9100-compliant optical inspection regimes (using Zygo GPI phase-shifting interferometers, Taylor Hobson surface profilometers, and spectrophotometric spectrophotometers).
Crucial Industrial Use-Cases & Environmental Demands
Where sapphire crystal outclasses all alternative glasses: harsh conditions, high optical flux, corrosive plasmas, and deep physical wear.
Semiconductor & Plasma Etch
In reactive ion etching (RIE) and inductively coupled plasma (ICP) chambers containing fluorine and chlorine chemistry (e.g., CF4, NF3), standard quartz erosion causes particulate contamination. Sapphire plasma viewports, lift pins, and dielectric wafer showerheads remain chemically inert, delivering 5× to 8× longer MTBF (mean time between failures).
High-Power Laser Debris Shields
Industrial multi-kilowatt fiber lasers (1064 nm) and high-fluence CO2/ultrafast lasers create massive thermal lensing inside low-conductivity glasses. Sapphire's exceptional thermal conductivity (35 W/m·K @ 25°C) rapidly dissipates spot heat, preventing catastrophic thermal rupture and self-focusing optical damage.
Aesthetic Laser & IPL Light Guides
Intense Pulsed Light (IPL) aesthetic handpieces demand optical wave blocks that transmit therapeutic visible/NIR wavelengths while filtering skin-damaging UV bands. Sapphire light guide blocks provide high thermal capacity to cool patient epidermis contact surfaces during high-joule flashlamp firing, ensuring painless cosmetic treatment.
Aerospace Sensor Domes & FLIR
Forward-Looking Infrared (FLIR) and missile tracking optical windows encounter supersonic rain erosion, sandstorm impact abrasion, and severe thermal shock when accelerating to Mach speeds. Sapphire's Young's modulus of 345–435 GPa maintains structural hermeticity and sensor optical clarity where optical zinc selenide (ZnSe) or germanium would pit and shatter.
Deep-Sea Oceanographic Viewports
For autonomous underwater vehicles (AUVs) and manned submersibles descending beyond 6,000 meters into abyssal trenches, hydrostatic pressure exceeds 60–110 MPa. Sapphire viewports permit thinner, lighter optical window profiles compared to bulky borosilicate glass, retaining 90%+ broadband transmission while resisting scratch damage from marine sediments.
Medical Diagnostics & Endoscopy
Rigid laparoscopes, arthroscopes, and analytical flow cells undergo repeated autoclaving cycles (134°C steam under high pressure) and abrasive enzymatic cleaning agents. Sapphire distal protective cover lenses prevent lens clouding, scratching, and hermetic seal leaks over thousands of sterilization cycles.
Global B2B Sourcing Protocol & Drawing Verification
Mitigate downstream yield losses by standardizing tolerance requirements, surface finish designations, anti-reflective coatings, and edge geometries.
Procuring custom sapphire optical parts from offshore manufacturing centers frequently encounters costly design interpretation errors. Unlike standard optical glasses where isotropic mechanical removal is predictable, sapphire's hardness (Mohs 9) and hexagonal cleavage planes can induce internal micro-cracks and latent stress fractures if machining parameters are ill-defined. Sourcing directors and chief optical engineers should implement the following qualification checkpoints:
The Surface Quality & Subsurface Damage (SSD) Trap
A common pitfall is over-specifying or under-specifying surface aesthetics. A drawing requesting "60-40 scratch-dig" per MIL-PRF-13830B may appear acceptable for industrial viewports. However, in high-power UV laser or cryogenic vacuum environments, coarse abrasive grinding that precedes final polishing leaves invisible subsurface fractures (SSD) reaching depths of 10–50 μm into the sapphire matrix. When irradiated by high-energy laser pulses, these micro-cracks act as localized thermal absorbers, triggering catastrophic optical breakdown (LIDT failure).
Sourcing Specification Rule: For precision optics, mandate Chemical Mechanical Planarization (CMP) with an Ra surface roughness ≤ 0.3 nm (measured via Atomic Force Microscopy / AFM) and clear confirmation of a damage-free subsurface structure verified by etching or phase-shifting interferometry.
Thin-Film Coating Adhesion on Corundum Substrates
Sapphire has a high refractive index (n ≈ 1.76 at 632.8 nm), causing roughly 7.7% Fresnel reflection per uncoated surface (14.8% total transmission loss across both window interfaces). To achieve >99% throughput, anti-reflective (AR) dielectric coatings must be deposited via Ion-Assisted Deposition (IAD) or Ion Beam Sputtering (IBS). Because sapphire has an extremely low coefficient of thermal expansion (5.3 × 10⁻⁶ /K parallel to c-axis), mismatch in thermal expansion with dielectric coating stacks (e.g., TiO2, SiO2, Ta2O5) can cause film delamination under thermal cycling.
Always specify coating operating temperature ranges (-50°C to +300°C) and enforce adhesion tape tests (MIL-C-48497A) as part of standard batch incoming inspection.
Because single-crystal sapphire is inherently brittle, sharp 90° external corners are highly vulnerable to chipping during assembly mounting. Always incorporate a minimum protective chamfer (0.1 mm to 0.3 mm × 45°) with fine-ground or polished bevels on manufacturing prints. Ground edges inhibit micro-crack propagation that leads to mechanical failure under hydrostatic or mechanical clamping loads.
Sapphire Industry Megatrends: 2026–2030 Roadmap
Emerging breakthroughs in crystal diameter scaling, direct femtosecond laser scribing, and hybrid crystal-to-metal vacuum brazing.
12-Inch (300mm) Large Aperture Wafers
Driven by advanced Silicon-on-Sapphire (SOS) microelectronics and next-generation Micro-LED display mass transfer platforms, manufacturing facilities are scaling automated Kyropoulos growth furnaces to yield flawless 12-inch monocrystalline ingots with minimal bubble-cloud cores and zero macroscopic lineage defects.
Femtosecond Laser Stealth Dicing
Mechanical blade sawing produces edge micro-chipping on hard sapphire. Emerging factories are deploying non-ablative infrared femtosecond laser pulses focused internally inside the sapphire lattice to induce multiphoton absorption. This creates localized micro-void lines (stealth dicing) that fracture cleanly with near-zero debris and ultra-high die strength.
Hybrid Direct Bonding & Brazing
Eliminating epoxy outgassing in ultra-high vacuum (UHV) instruments, optical factories are perfecting direct surface-activated bonding (SAB) of sapphire to fused silica, silicon, and specialized titanium/Kovar metal flanges via reactive active metal brazing (AMB), producing hermetic joints stable from cryogenic 4K to over 800°C.
Semiconductor Quartzware, Flowcells & Optical Ferrules
Complementary precision-engineered components manufactured under one roof: UV-grade fused silica, doped laser cavities, and ceramic components.
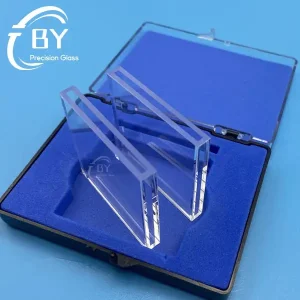
Wholesale Customize Quartz Cuvette for Spectrophotometer Supplier, Factory
Explore Product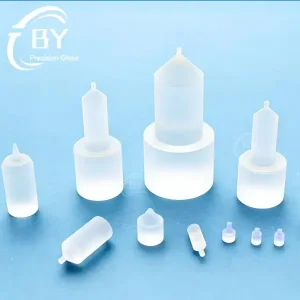
High-Quality Customized Quartz Fiber End Caps for QBH Manufacturer, Factory
Explore Product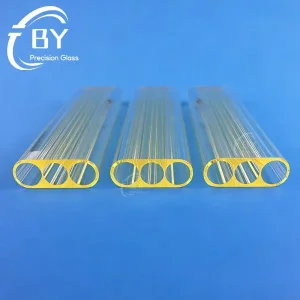
Custom Laser Cavity Flow Tubes & Filters Made from Samarium-doped Glass Supplier, Suppliers
Explore Product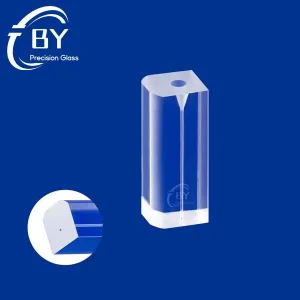
Custom Fiber Optic Glass Ferrules Supplier, Factories
Explore Product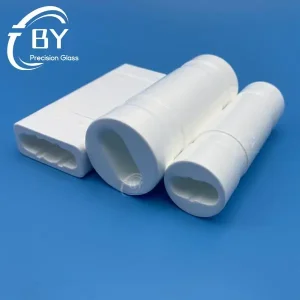
Wholesale Ceramics Reflecor for Semiconductor Lasers Suppliers, Factory
Explore Product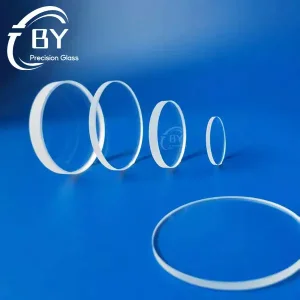
Wholesale Quartz Optical Windows for Semiconductor Lithography Equipment Suppliers, Factories
Explore Product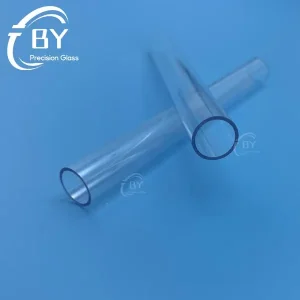
Wholesale Cerium Doped Quartz Tube Blocked UV Wavelength Manufacturer, Manufacturers
Explore Product
High-Quality Precision Custom Quartz Glass Components for Semiconductor Manufacturers, Supplier
Explore ProductFrequently Asked Questions (FAQ) for Engineering Buyers
Authoritative technical answers to assist procurement engineers, optical designers, and sourcing teams when specifying custom sapphire and quartz components.