
Featured Optical & Laser Core Components
Engineered alongside our sapphire light guide processing lines, these precision quartz, ceramic, and optical components deliver unmatched durability across high-power laser and semiconductor architectures.
Why Sapphire (Single-Crystal Al₂O₃) Dominates Modern Light Guides
Unlike standard fused silica or BK7 optical glasses, single-crystal sapphire offers a unique combination of optical transparency across UV-Vis-NIR (170 nm to 5500 nm), unparalleled mechanical rigidity, and unmatched thermal conductivity.
Contact Cooling & Heat Dissipation
In medical aesthetic systems like IPL and high-fluence 808nm diode arrays, patient skin safety relies on immediate contact epidermal cooling. Sapphire delivers a thermal conductivity of ~35–42 W/m·K—nearly 30 times higher than fused silica (1.38 W/m·K). This allows Peltier thermoelectric elements to maintain crystal tip temperatures below 0°C even during rapid 10 Hz pulse operation.
Total Internal Reflection (TIR) Fidelity
With a high refractive index of n ≈ 1.76 at 633 nm, sapphire provides a steep critical angle (θc ≈ 34.6° against air). Light injected from flashlamps or diode laser bars is reflected repeatedly across polished longitudinal side facets via total internal reflection, functioning as an ideal optical homogenizer that converts Gaussian hot spots into uniform flat-top output profiles.
Abrasion & Chemical Inertness
With a Mohs hardness of 9 (second only to diamond), sapphire light guides resist abrasive coupling gels, clinical alcohol cleaners, and micro-particle bombardment during rigorous clinical or industrial laser cycles. The optical surfaces retain sub-micron roughness (Ra < 0.5 nm) over years of clinical sterilization without haze, clouding, or solarization degradation.
Engineering Benchmark: Sapphire vs. Fused Silica vs. N-BK7 vs. Quartz
For optical system integrators and laser equipment OEMs, choosing the correct light guide substrate dictates transmission efficiency, thermal runaway margins, and component life under pulsed laser fluences.
| Material Substrate | Transmission Bandwidth | Refractive Index (nd) | Thermal Conductivity | Mohs Hardness | LIDT Laser Damage Threshold | Primary Industrial Use-Case |
|---|---|---|---|---|---|---|
| Monocrystalline Sapphire (Al₂O₃) | 170 nm – 5,500 nm | 1.768 | 35 - 42 W/m·K | 9 Mohs | > 25 J/cm² @ 1064nm, 10ns | IPL skin cooling, high-duty aesthetic handpieces, harsh sensors |
| UV Synthetic Fused Silica (JGS1) | 185 nm – 2,500 nm | 1.458 | 1.38 W/m·K | 6.5 - 7 Mohs | > 40 J/cm² @ 1064nm, 10ns | Excimer lasers, deep UV lithography, high-fluence fiber tips |
| Optical Fused Quartz (JGS2) | 220 nm – 2,500 nm | 1.458 | 1.40 W/m·K | 6.5 Mohs | ~ 15 - 20 J/cm² @ 1064nm | Standard laser flow tubes, furnace viewports, lamp sleeves |
| Low-OH Infrared Quartz (JGS3) | 260 nm – 3,500 nm | 1.458 | 1.40 W/m·K | 6.5 Mohs | ~ 15 J/cm² @ 1064nm | Mid-IR spectroscopy, infrared optical couplers, pyrometry |
| Optical Crown Glass (N-BK7) | 350 nm – 2,000 nm | 1.517 | 1.11 W/m·K | 5.5 Mohs | ~ 8 - 10 J/cm² @ 1064nm | Low-power commercial optics, machine vision prism blocks |
*Note: Thermal conductivity values measured at 25°C. Sapphire exhibits slight anisotropic variations between C-plane [0001] and A-plane [11-20] orientations. Our facility accommodates customized crystal axis alignments.
The Strategic Advantages of Sourcing Wholesale Sapphire from China
Tianjin BY Photonics bridges world-class crystal growth technology with high-precision CNC multi-axis fabrication, offering tier-1 international OEMs scalable output, cost efficiency, and rigorous quality traceability.
Vertically Integrated Supply Chain
China is home to the world's largest synthetic sapphire ingot crystal-pulling infrastructure (Kyropoulos & Heat Exchanger methods). We procure prime optical-grade boule material with zero bubble inclusions, low stress birefringence, and homogeneous lattice structures at direct factory rates.
Sub-Micron Diamond CNC Polishing
Machining single-crystal sapphire demands extreme tool rigidity. Our 120+ processing machines include 5-axis ultrasonic CNC diamond profiling stations and double-sided planetary pitch polishers capable of reaching scratch-dig tolerances down to MIL-PRF-13830B 20-10.
In-House PVD/IAD Dielectric Coating
We apply high-density electron beam ion-assisted deposition (IAD) coatings directly on sapphire ends. Our anti-reflective (AR) coatings (single, dual, or broadband wavelengths) achieve reflectance R < 0.25% per surface while withstanding intense thermal cycles without cracking.
Metrology & Cleanroom QC
Every wholesale batch undergoes 100% inspection using Zygo laser interferometers for transmitted wavefront error, Olympus optical surface microscopes for scratch-dig analysis, and coordinate measuring machines (CMM) for precision bevel profiling.
Localized Application Scenarios & Macro Industry Solutions
Sapphire light guides act as the frontline interface between photon-generation sources and mission-critical targets across diverse optical ecosystems.
Medical Dermatology & IPL Handpieces
In Intense Pulsed Light (IPL), SHR, and 808nm / 755nm / 1064nm hair-removal devices, the sapphire light guide prism channels energy into targeted follicular melanin while cooling the epidermal surface. Our high-precision chamfered light blocks prevent epidermal burns caused by perimeter edge leakage or focal pinching.
High-Fluence Industrial Beam Homogenizers
For laser plastic welding, metal hardening, and industrial marking, Gaussian laser beams create localized overheating. Hexagonal and rectangular sapphire homogenizing rods utilize non-imaging optics to scramble modes, producing homogeneous top-hat energy profiles with uniform cross-sectional intensity.
Rigid Endoscopy & In-Vivo Surgical Tools
Surgical endoscopes demand miniature light guides with micro-diameters (down to Ø 0.8 mm) that withstand repeated autoclave steam sterilization at 134°C. Sapphire's chemical inertness prevents clouding under alkaline enzymatic detergents and high-pressure steam autoclaves.
Aerospace & Downhole Optoelectronic Sensors
Deployed in extreme-temperature turbine diagnostics, deep-well borehole oil exploration, and flight-control instrumentation, our sapphire optical waveguides transmit signals reliably under pressures exceeding 10,000 psi and ambient temperatures spanning -60°C to +800°C.
Semiconductor Lithography & UV Photolithography
Used to guide UV and deep UV exposure flux during wafer-level photolithography alignment and UV polymer adhesive curing. Sapphire avoids color center degradation (solarization) that plagues borosilicate and common optical glasses under short-wavelength UV rays.
Turnkey Optomechanical Housing & Brazing
Thermal mismatch between sapphire (CTE ~5.8×10⁻⁶/K) and metal housings can cause adhesive failure or fracture. BY Photonics offers turnkey hermetic metallization (gold/nickel sputter coating) and high-temperature brazing to Kovar, Invar, and titanium sleeves.
Global B2B Sourcing Demands: What Tier-1 OEMs Require
Procuring sapphire light guides at scale requires engineering rigor. When submitting RFQs to our manufacturing floor, specifying these key manufacturing parameters ensures zero tolerance drift and rapid mass production.
1. Surface Quality & Roughness
Light guides have two critical optical interfaces: the end input/output faces and the longitudinal TIR side faces. End faces typically require 20-10 or 40-20 Scratch-Dig with roughness Ra < 0.5 nm to eliminate scatter loss. Side faces can be polished for total internal reflection or precision-frosted/lapped (fine-ground) when controlled side-emission or diffuse mixing is required.
2. Perimeter Edge Beveling & Micro-Chamfering
Because sapphire possesses high crystal hardness, unchamfered 90° edges are prone to micro-chipping during transport, laser mounting, or clinical contact. Our standard specification includes a 45° protective micro-chamfer (0.1 mm to 0.3 mm) polished to optical smoothness to eliminate localized stress risers and protect skin contact safety.
3. Anti-Reflective (AR) Thin-Film Design
With an index of n ≈ 1.76, an uncoated sapphire face reflects approximately 7.6% of incident light per surface (Fresnel reflection loss). Wholesale buyers frequently request custom AR coatings: single-band (e.g., 808 nm for diode lasers, 1064 nm for Nd:YAG), dual-band (755/1064 nm for alexandrite/YAG systems), or broadband AR (400–1200 nm for broad spectrum IPL).
4. Geometric & Angular Tolerances
Whether configuring tapered light guides (concentrators) for fluence amplification or rectangular prisms for beam delivery, dimensional tolerances must be kept within ±0.02 mm (standard) to ±0.005 mm (ultra-precision). Parallelism between opposite faces should remain < 30 arcseconds, and perpendicularity within < 1 arcminute to preserve beam trajectory.
5. Bubble Classes & Crystal Orientation
Standard light guides are machined along the C-plane [0001] axis to prevent birefringence-induced double refraction along the primary optical path. For polarized laser transmission, specific A-plane [11-20] or R-plane [1-102] orientations can be chosen to maintain polarization purity. All bulk raw materials comply with zero visual bubble and seed inclusions.
6. Cleanroom Packaging & Lot Traceability
Every wholesale shipment is ultrasonically degreased, deionized-water rinsed, and packaged in Class 1000 cleanroom environments. Parts are individually sealed in dust-free membrane boxes or vacuum-sealed ESD-safe trays, accompanied by raw material melt certificates and CMM dimensional inspection protocols.
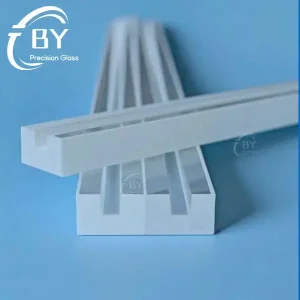
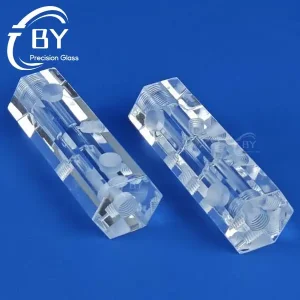
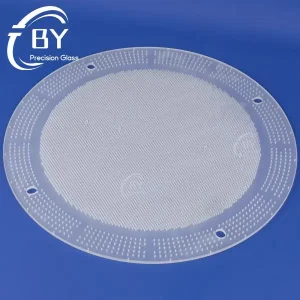
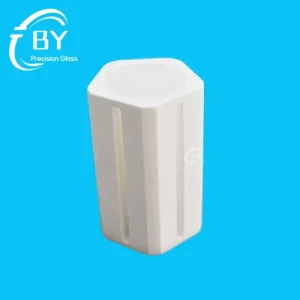
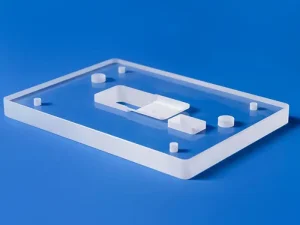
Comprehensive Optics & Semiconductor Quartzware
Complementing our sapphire light guide prisms, explore our advanced quartz substrate, reflector cavities, and high-purity optical components built for leading optoelectronic and laser system builders.
Frequently Asked Questions: Sapphire Light Guides
Detailed technical answers to common queries faced by procurement heads, optical system designers, and medical device engineers.
Request Engineering Feedback & Wholesale Pricing
Send us your 2D engineering drawings (PDF / DWG / DXF) or 3D models (STEP / IGES). Our senior optics engineers evaluate manufacturability, crystal orientation, coating curves, and deliver a comprehensive formal quote within 24 hours.
Consult With an Optical Engineer