Featured Product Showcase
High-Precision Machined Quartz & Optical Components
Engineered cold and hot-working components manufactured strictly to engineering prints for semiconductor, industrial laser, and analytical instrumentation applications.
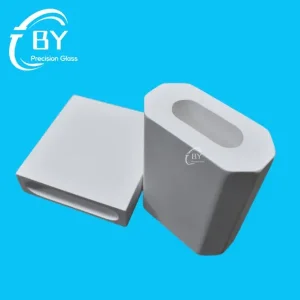
High-Quality Diffuse Reflectors Made of Spectralon-Grade PTFE for Diode-Pumping Chambers Manufacturer, Suppliers
View Product Details →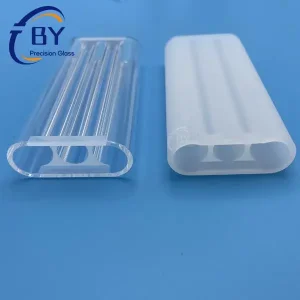
High-Quality Candela Laser Head Triple Bore Old and New Version In Stock Manufacturer, Factory
View Product Details →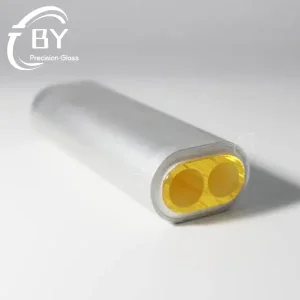
Custom Packed Laser Cavity Flowtubes for Laser Head Manufacturers, Suppliers
View Product Details →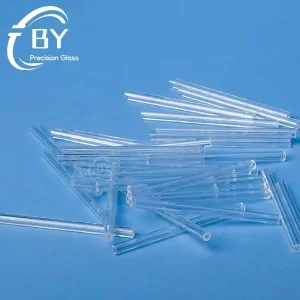
High-Quality Custom Precision Quartz Capillary Tubes Manufacturers, Suppliers
View Product Details →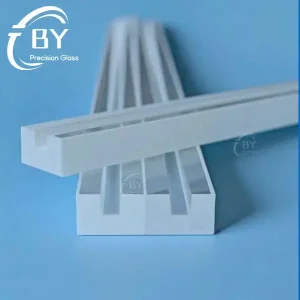
High-Quality Square Groove Quartz Substrate for Fiber Couplers Supplier, Factories
View Product Details →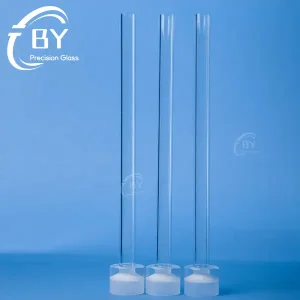
High-Quality Chemical Resistant Custom Quartz Glass Parts Fabrication Supplier, Factories
View Product Details →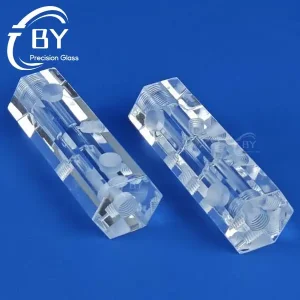
High-Quality Custom Fabrication of Quartz Glass Precision Components Supplier, Factory
View Product Details →
Industry Engineering White Paper
Global State of Quartz Machining Parts in High-Tech Manufacturing
Fused silica and high-purity synthetic quartz have evolved from standard laboratory glass into indispensable structural materials powering advanced photolithography, wafer processing, and ultra-fast laser systems.
99.999%
SiO2 Ultra-High Purity
±0.002mm
Micro-CNC Tolerance
1,150°C
Continuous Thermal Ceiling
λ/10
Interferometric Surface Flatness
Severe Operating Demands
Modern semiconductor fabrication plants (fabs) operate under extreme plasma dry-etch chemistry (CF4, NF3) and rapid thermal processing cycles. Traditional borosilicate glass suffers mechanical failure and ionic leaching; machined synthetic quartz provides zero chemical erosion and absolute lattice stability.
Near-Zero Thermal Expansion
With an extraordinarily low thermal expansion coefficient (α ≈ 5.5 × 10^-7 / °C), precision quartz components maintain dimensional integrity even during abrupt temperature fluctuations from ambient room temperature to over 1,000°C, preventing cavity misalignments in laser heads.
Deep Spectral Transmission
From Deep Ultraviolet (DUV 193nm) photolithography lenses to Far-Infrared spectroscopy, synthetic JGS1, JGS2, and JGS3 quartz variants deliver broad spectral transmission and near-zero fluorescence, outperforming nearly all other optical ceramics.
Direct Factory Capabilities
Integrated Engineering & Supply Chain Dominance
Combining cold abrasive processing and hot flame restructuring under one roof eliminates outsourcing delays and prevents inter-facility micro-fracturing.
Full In-House Workcell
Over 120 precision processing units including 4-axis/5-axis ultrasonic CNC diamond milling, double-sided planetary lapping machines, and automated redraw towers.
- No subcontractor margin stack
- Direct material custody tracking
- Rapid re-tooling in under 24 hours
70% Faster Turnaround
By keeping raw ingot stockpiles (JGS1, JGS2, JGS3, Corning 7980, and Spectrosil equivalents), prototypes ship within 7–10 days rather than 8–12 weeks typical of Western suppliers.
- Immediate DFM design verification
- In-stock certified optical blanks
- Express global air freight packaging
Sub-Surface Crack Elimination
Hard and brittle crystal grinding can induce latent subsurface micro-cracks. Our specialized chemical-mechanical etching and thermal annealing alleviate internal crystal tension completely.
- Polariscopic stress verification
- Controlled acid etching finish
- Vacuum thermal anneal cycles
Comprehensive Metrology
Equipped with Zygo VeriFire laser interferometers, Mitutoyo CNC coordinate measuring machines (CMM), and PerkinElmer Lambda UV/Vis/NIR spectrophotometers.
- 100% dimensional inspection reports
- Surface roughness Ra down to 0.5nm
- Optical transmittance validation
Technical Material Matrix
Engineering Grade Selection Guide for Custom Quartz Parts
Selecting the optimal fused silica grade balances spectral transmission requirements, hydroxyl [OH-] radical absorption, and mechanical durability.
| Material Grade | Transmission Band | Hydroxyl [OH-] Content | Bubble / Inclusion Class | Primary Industrial Applications |
|---|---|---|---|---|
| JGS1 (Synthetic UV Silica) | 185 nm – 2,500 nm | ≤ 1000 ppm | Class 0 (Bubble-free optical) | DUV laser windows, spectroscopy cuvettes, high-power beam splitters, photolithography. |
| JGS2 (Optical Fused Quartz) | 220 nm – 2,500 nm | ≤ 200 ppm | Class 1 / Class 2 | Semiconductor wafer boats, sight glass, laser cavity flow tubes, furnace liners. |
| JGS3 (Infrared Grade Silica) | 260 nm – 3,500 nm | ≤ 5 ppm (Water-free) | Class 1 (Ultra-low OH) | Thermal imaging viewports, IR laser chambers, atmospheric sensors, military optical shells. |
| Cerium / Samarium Doped | Custom cutoff bands | Standard | Class 1 | Solid-state Nd:YAG flashlamp flowtubes, dermatological IPL handpieces, UV cutoff filters. |
| Fluorine-Doped Quartz | Low-index optical band | Low OH options | Capillary precision grade | Fiber optic ferrule blanks, microfluidic chips, capillary electrophoresis capillaries. |
Localized Application Scenarios
Where Precision Machined Quartzware Delivers Critical Value
Across cleanrooms, surgical suites, and laser industrial automation, BY Photonics custom-engineered quartz parts ensure failure-free execution.
1. Semiconductor Wafer Processing
In LPCVD, PECVD, and dry diffusion furnaces, our wafer carriers and diffusion boats endure corrosive chemical clouds at 1,100°C without warping. Flawless oxyhydrogen flame welding ensures quartz joints maintain vacuum seal integrity under thermal expansion strain.
2. High-Duty Solid-State Lasers
Candela-compatible triple bore cavities, Nd:YAG cooling jackets, and packed samarium flowtubes selectively suppress parasitic 1064nm amplified spontaneous emission while protecting the laser medium with coolant channels bored to 20-micron concentricity.
3. Aesthetic & Medical IPL Systems
Cerium-doped quartz tubes and sapphire light guide blocks filter destructive ultraviolet rays below 380nm from xenon flashlamps. This preserves cosmetic handpiece casing longevity and eliminates tissue burn risks during laser hair removal and skin rejuvenation.
4. Fiber Couplers & Telecommunications
Micro-structured square groove quartz substrates enable v-groove fiber alignment array packages down to sub-micron channel spacing, crucial for telecom transceivers, DWDM systems, and polarization-maintaining fiber couplers.
5. Analytical Chemistry & Bio-chips
Spectroscopic flow cells and fused silica microcapillaries boast internal surface roughness below Ra 1nm. Non-reactive, hydrophobic surfaces prevent sample carryover in capillary electrophoresis, HPLC detectors, and blood sequencing apparatus.
6. High-Temperature Furnace Viewports
Thick-section custom quartz sight glasses, flanged viewport covers, and vacuum tube ends engineered to withstand up to 10 bars of positive pressure and continuous high thermal cycling without devitrification or clouding.
Strategic Trends
Emerging Trends & What Global Procurement Teams Prioritize
Strategic buyers from North America, Europe, and Asia-Pacific demand more than low unit costs. Technical competence, drawing confidentiality, and end-to-end quality documentation define vendor qualification.
1. Cleanroom Packaging & Ready-to-Install Parts
Modern fab lines refuse to clean incoming quartzware due to solvent residue risks. Tier-1 buyers require class 10,000 cleanroom ultrasonic washing, vacuum triple-bag packaging, and ion-free nitrogen flushing so components drop directly into vacuum chambers.
2. Precision Hybrid Multi-Material Assemblies
Standalone quartz machining is evolving into hybrid component integration. OEMs seek factories able to fuse quartz to Kovar, combine Spectralon-grade diffuse PTFE with samarium glass cooling filters, and solder metal flanges to metallized quartz rings.
3. Complete Traceability & Metrology Proof
Procurement audits demand batch certificates for raw fused silica ingots, refractive index homogeneity mappings, trace bubble/inclusion grades, and 3D CMM inspection data cards delivered with each serial-numbered part.
Engineering Helpdesk
Frequently Asked Questions on Custom Quartz Machining
Clear, technical explanations to support your procurement, manufacturing tolerance evaluations, and drawing releases.
What is the standard tolerance achievable on CNC machined quartz?
For general CNC milled features (pockets, steps, contours), we maintain ±0.05 mm routinely. On critical ground and lapped dimensions, bore centerlines, and optical flats, our tolerances reach ±0.005 mm to ±0.002 mm, verified via laser interferometry and 3D CMM.
How do you prevent micro-cracking and thermal stress in quartz welding?
All hot-worked quartz assemblies (such as wafer boats and fused manifold pipes) undergo high-temperature oxyhydrogen flame manipulation followed by precision electric furnace annealing cycles up to 1,150°C. Slow controlled cooling relieves residual internal lattice tension, preventing catastrophic failure under thermal cycling.
Which drawing files are required for an engineering quote?
We accept 3D CAD models (STEP, IGES) alongside 2D engineering drawings (PDF, DWG, DXF). The 2D drawings must specify critical tolerance thresholds, surface roughness requirements (Ra or Scratch-Dig), edge chamfers, and clear material grades (JGS1, JGS2, JGS3, or borosilicate).
Can you provide custom anti-reflective (AR) and metallic coatings on quartz?
Yes. In addition to precision CNC machining and optical polishing, our facility provides Ion-Assisted Deposition (IAD) thin-film coating services, including UV-AR, NIR-AR, dual-wavelength antireflective, and metal mirror coatings (Gold, Silver, Aluminum) adhering strictly to MIL-PRF-13830B standards.
What is the typical prototype lead time versus volume production?
For rapid prototypes where stock ingot materials are available, engineering evaluation and part shipment takes 7 to 10 working days. Commercial batch production (100 to 5,000+ units) typically finishes within 3 to 4 weeks depending on optical coating and metrology requirements.
How do you guarantee safe delivery of brittle quartz components globally?
Every fragile quartz part is individually sealed in static-free vacuum film, cushioned in custom CNC-cut high-density shock-absorbing EPE foam pods, and packed within shock-isolated, reinforced export wooden crates equipped with drop/tilt indicator monitors.
Complete Range Catalog
Specialized Quartz, Silica & Sapphire Components
Browse our extensive production line of customized semiconductor quartzware, laser pumping chambers, and optical light guides ready for volume production.
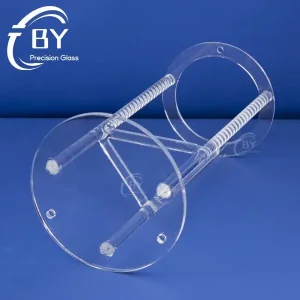
Wholesale Quartz Wafer Carriers for Semiconductor Supplier, Suppliers
View Product Details →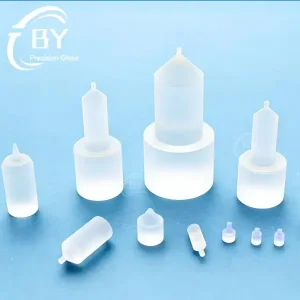
High-Quality Customized Quartz Fiber End Caps for QBH Manufacturer, Factory
View Product Details →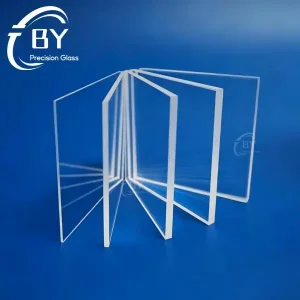
High-Quality JGS1 UItraviolet (UV) Grade Fused Silica Plate Supplier, Factory
View Product Details →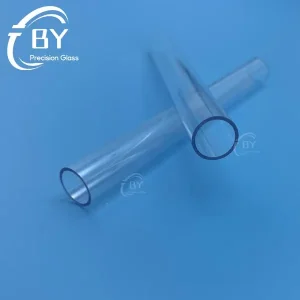
Wholesale Cerium Doped Quartz Tube Blocked UV Wavelength Manufacturer, Manufacturers
View Product Details →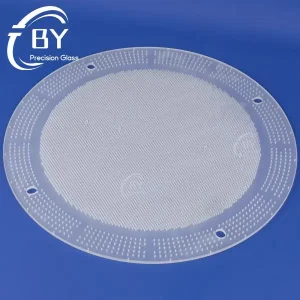
Custom Custom Optical Quartz Gas Distribution Plate Manufacturer, Suppliers
View Product Details →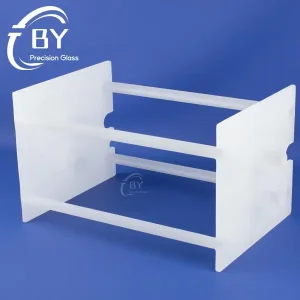
Wholesale Quartz Diffusion Boat for Semiconductor Suppliers, Factories
View Product Details →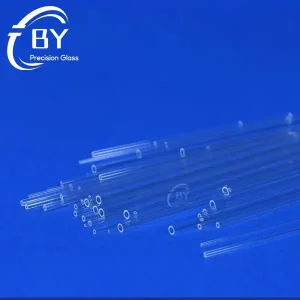
Wholesale Fluorine-Doped Fused Silica Capillary Tube Manufacturer, Factories
View Product Details →