Precision Optical & Cavity Components (Catalog 1-8)
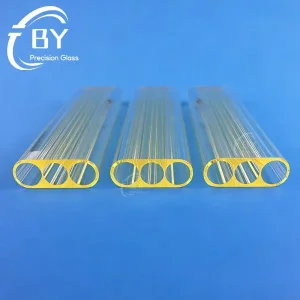
Direct factory manufacturing of laser cavity flow tubes, UV synthetic quartz, and advanced diffuse reflectors integrated directly into high-power laser delivery chains.
Industrial White Paper: High-Power Fiber End Caps for QBH Architecture
Analysis of optical physics, thermo-mechanical endurance, and material purity parameters determining failure thresholds in fiber connector interfaces operating at 1 kW to 30 kW+ power levels.
Beam Expansion & Surface Intensity Mitigation
High-power fiber lasers output extreme power densities through micro-scale fiber cores. A 50 μm core transporting 12 kW results in power densities exceeding hundreds of megawatts per square centimeter. A synthetic fused silica end cap (JGS1) fusion-spliced to the fiber termination allows the guided mode to diverge freely into bulk quartz before hitting the air-glass boundary. By spreading the beam spot size by orders of magnitude, power density at the optical face drops below critical damage thresholds, preventing catastrophic end-face ablation and localized plasma ignition.
Sub-Surface Damage & Advanced Magnetorheological Finishing
Standard mechanical polishing leaves micro-fractures, polishing slurry entrapped within subsurface fissures, and structural micro-voids that induce premature thermal runaway. Our QBH end caps undergo super-polishing paired with chemical-mechanical polishing (CMP) and ion-beam profiling. The resulting sub-angstrom surface roughness (Ra < 0.5 nm) completely eradicates subsurface damage (SSD). This process achieves an exceptional Laser-Induced Damage Threshold (LIDT > 45 J/cm² @ 1064 nm, 10 ns), critical for continuous multi-kilowatt CW lasers.
Dielectric Coating & Back-Reflection Management
In industrial cutting and welding of highly reflective non-ferrous alloys (copper, brass, aluminum), back-reflected radiation can re-enter the fiber core, destabilizing laser resonators and destroying pump combiners. Our QBH end caps feature proprietary ion-assisted deposition (IAD) anti-reflective coatings (AR @ 1064 nm, 1030-1080 nm, or dual-band 1064/635 nm for pilot laser alignment). This achieves an ultra-low reflectance (R < 0.1%), low thermal absorption (thermal drift < 0.5 μrad/W), and withstands extreme industrial operating cycles.
China Factory Supply Chain & Global Sourcing Architecture
How our integrated raw synthetic quartz supply, in-house precision cold/hot processing, and international compliance deliver unrivaled scalability for OEM photonics developers.
End-to-End Vertical Integration
Unlike trading intermediaries, BY Photonics houses the entire workflow in Tianjin: synthetic raw boule selection, wafer cutting, CNC cylindric profiling, double-sided super-polishing, ultrasonic class 100 cleaning, and optical vacuum sputtering. This eliminates subcontract markups and provides total traceability down to material lot melt data.
Global Regulatory Compliance
All synthetic fused silica fiber end caps and QBH components comply with RoHS 3 (EU 2015/863), REACH (EC 1907/2006), and ISO 9001:2015 production quality assurance. Surface inspections meet the exacting standards of MIL-PRF-13830B and ISO 10110 for international optical component integration across Europe, North America, and APAC.
Agile Rapid Prototyping
Our dedicated engineering quick-turn line can produce customized dimensional end caps (e.g., diameters from 2 mm to 15 mm, custom lengths from 5 mm to 30 mm, with or without anti-reflective bevels) within 5–7 working days, facilitating rapid iterative R&D cycles for emerging 20 kW to 60 kW fiber laser sources.
Rigorous Optical Metrology
Every batch of fiber end caps is verified using Zygo Verifire laser interferometers for transmitted wavefront distortion, atomic force microscopy (AFM) for surface microroughness, and automated spectrophotometers to ensure absorption values are maintained below 5 ppm/cm at the 1064 nm wavelength.
Emerging Trends & Advanced Industrial Application Scenarios
The laser industry's migration toward ultra-high brightness, beam-shaping outputs, and multi-wavelength processing is driving new demands for fiber end cap design.
Sheet Metal Cutting (30 kW to 60 kW)
The rapid deployment of 30 kW+ ultra-high-power fiber cutting heads requires QBH end caps with thermal focus shift properties near zero. Reduced OH content synthetic quartz (JGS1) guarantees minimal heat absorption, ensuring consistent focal positioning during continuous thick-plate carbon steel and stainless steel processing.
E-Mobility Hairpin & Battery Welding
Automotive battery welding requires ring-mode or adjustable beam profile (core-ring dual beam) delivery. Our specialized composite end caps support multi-clad fibers, allowing core and ring power balancing without thermal distortion or interfacial micro-cracking during deep-penetration copper busbar welding.
Aerospace Laser Cladding & Additive Manufacturing
Extreme-speed laser additive deposition processes subject delivery optics to continuous high-duty-cycle thermal feedback, airborne powder, and high ambient temperatures. BY Photonics QBH quartz assemblies feature chemically inert coatings and superior heat-shock tolerance up to 1100°C.
Need Custom Fiber End Cap Specifications for Next-Gen Laser Heads?
Our optical fabrication engineering desk provides complete technical assessments within 24 working hours. Send your custom prints, power targets, and mechanical envelopes directly to our team.
Frequently Asked Questions (Technical & Procurement FAQ)
Clear technical answers addressing critical parameters, material specifications, and engineering considerations for QBH fiber end cap integration.
Engineered Glass, Ceramics & Reflectors (Catalog 9-16)
Explore our expanded range of laser cavities, ceramic reflectors, borosilicate sight windows, and high-purity optical components built to exact customer drawings.